The processing of "Big Red" stone involves multiple stages, ranging from quarrying raw blocks to packaging the finished product; specific workflows vary depending on the stone variety and intended application. The following is a systematic overview covering raw block sawing, grinding and polishing, cutting and shaping, red-dyeing, surface treatment, auxiliary processing, and inspection and packaging.
Raw Block Sawing
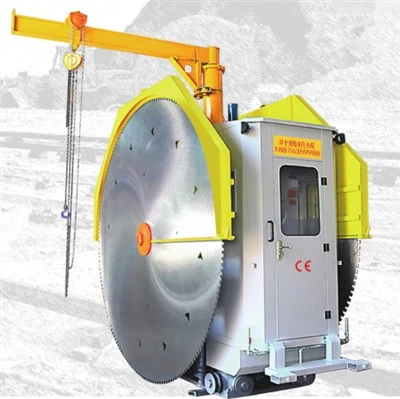
Sawing is the fundamental process of cutting natural granite blocks into semi-finished products such as rough slabs, strips, or blocks. As a rough processing stage, it directly impacts slab yield, quality, and the enterprise's economic efficiency. Common sawing equipment includes large automatic frame saws (using abrasive sand) designed specifically for granite, multi-blade bidirectional cutters, computer-controlled multi-blade granite cutters, and granite circular saws. Rough slabs typically have a thickness of 15 mm or 20 mm. Wet processing is generally employed during cutting, with water spraying used to minimize dust generation. After sawing, the rough slabs are washed and inspected for obvious cracks or defects.
Grinding and Polishing
The purpose of grinding and polishing is to further process the sawn rough slabs to meet specific requirements regarding thickness, flatness, and gloss. This process typically proceeds in stages: coarse grinding, semi-fine grinding, fine grinding, precision grinding, and polishing. The coarse grinding stage begins with leveling, followed by successive grinding steps that fully reveal the granite's color and texture. Key equipment includes automatic multi-head continuous grinding machines, diamond leveling machines, bridge-type grinders, rotary disc grinders, reversing coarse grinders, and handheld grinders. For dyeable "Big Red" stone, some processes involve grinding the slab to a gloss level of approximately 60 to 70 degrees to prepare it for subsequent dyeing.
Cutting and Shaping
Cutting involves using a cutting machine to shape rough or polished slabs into the required dimensions and specifications. This stage transforms large slabs into sized tiles or panels that meet specific order requirements. Common cutting equipment includes longitudinal multi-blade saws, transverse saws, bridge saws, cantilever saws, and manual saws. For products requiring special shapes, additional processing such as profile milling and drilling can be performed. The cutting sequence generally follows the principle of processing smaller dimensions before larger ones.
Dyeing Process
The processing steps for granite slabs requiring a red finish via dyeing are relatively complex. First, the cut and ground slabs are placed in an oven for drying. The drying temperature is typically controlled between 145°C and 205°C, with a duration of 1 to 4 hours. Once dried, the slabs are fully immersed in a prepared dyeing solution (such as ferric chloride or ferric nitrate). The immersion time-usually 2 to 4 hours-is determined by factors such as the stone variety, desired color, and water absorption rate. After immersion, the slabs are removed and placed in a kiln for firing to develop the color; the firing temperature is usually between 130°C and 160°C, with a holding time of 2 to 3 hours. The immersion and firing processes may be repeated depending on the desired color depth. Upon completion of dyeing, the slabs undergo cleaning and a final polishing.
Surface Treatment
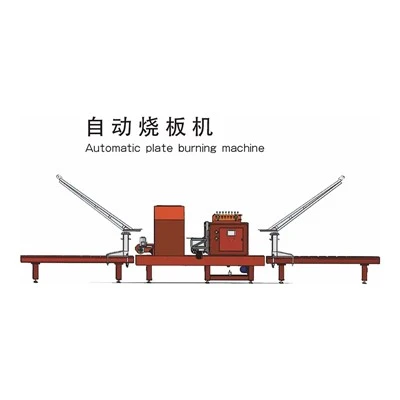
Various surface treatments can be applied to the stone based on usage requirements. A polished finish is achieved through grinding and polishing to create a mirror-like surface. A flamed finish (also known as thermal texturing) utilizes the differing thermal expansion coefficients of the minerals within the granite; a flame causes surface particles to expand, fracture, and flake off, creating a textured, rugged surface with a regular pattern. Finishes such as bush-hammered (lychee), natural cleft, and sandblasted are achieved through chiseling or mechanical processing. Additional options include matte, axe-hewn, machine-planed, and brushed finishes. Different surface treatments impart distinct visual and tactile qualities, making the stone suitable for various decorative applications.
Auxiliary Processing
Auxiliary processing refers to the subsequent treatment of stone slabs that have already been cut to size and polished. This includes processes such as edge grinding, chamfering, cutting openings, drilling holes, milling grooves, and edge profiling. Key equipment includes automatic edge-grinding and chamfering machines, profile milling machines, thin-wall drilling machines, handheld diamond circular saws, and handheld grinding and polishing machines. For products requiring assembly or splicing, processes such as layout planning, color matching, and numbering are necessary to ensure color and tone consistency across the installation surface.
Inspection and Packaging
Natural granite inevitably contains inherent flaws like cracks and voids, and minor defects such as nicks or abrasions may occur during processing. All finished slabs must undergo inspection. Inspection criteria cover visual quality (pattern and color tone), dimensional accuracy (e.g., perpendicularity and edge length), and gloss levels. Slabs are first cleaned, then air-dried and subjected to a comprehensive inspection. Products with minor defects that still meet order specifications may undergo adhesive repair to minimize waste. Qualified products receive protective treatment before being packaged and warehoused. Packaged products are then transported and delivered in accordance with order requirements.
Stone flaming involves multiple processing stages; from the sawing of raw blocks to the packaging of finished goods, every step impacts the quality of the final product. In actual production, appropriate processing techniques and surface treatments should be selected based on the specific characteristics of the stone variety and customer requirements.